
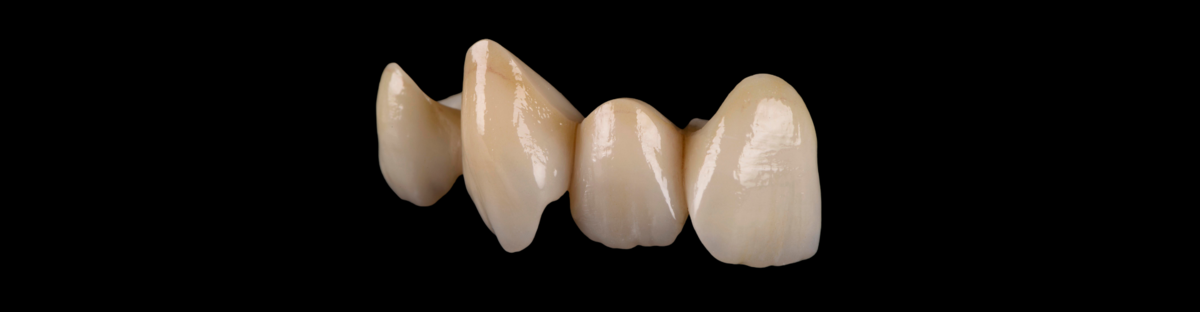
priti®multidisc ZrO2, Multi Translucent MZRB2016
Pritidenta GmbH · #MZRB2016
Collecté automatiquement depuis pritidenta.com
Vous êtes le fabricant ?Transmettez vos données
Texte du fabricant en anglais
What makes priti®multidisc ZrO2 Multi Translucent so special?
Following popular demand, this blank combines the positive properties of the already established zirconium dioxide qualities 3Y-TZP and the highly translucent 5Y-TZP in the enamel and in the body. Maximum safety? A scientific study proves it.
Indications
Our strong multi-talent can be used for all indications. Highly aesthetic monolithic, full-anatomical crowns, partial crowns and bridges up to 14 units, inlays, onlays, veneers and abutments. Its natural aesthetics and high stability make it suitable for the anterior and visible tooth region. In addition, the cervical opaque zirconium dioxide has good masking qualities. All processing techniques: Staining, cut-back and veneering techniques are possible. The combination of 3Y-TZP (Translucent with very high strength) and 5Y-TZP (High Translucent with very high translucency) gives a highly aesthetical effect and reliable strength for an unrestricted range of indications. In addition to a smooth transition between the layers within the blank or restoration, this product also has good masking qualities and high stability throughout the blank. The smooth transition between the layers results in a gradual progression of strength within the blank or restoration. Multi Translucent is therefore suitable for a wide range of indications.
Material
- Bending strength: typical mean value > 1,440 MPa
- top layer: > 980 MPa
- bottom layer: > 1,680 MPa
- Translucency gradient from > 40% to > 49%
- Thin wall thicknesses of 0.4 mm in the anterior region and 0.6 mm in the posterior region for single crowns
- Precise margins and edges due to highly compressed material
- Cross-batch shade fidelity
- Homogeneous staining
- Consistently reproducible shades
- Biocompatible
Application
In order to achieve optimum results and avoid errors, correct application is very important.
Construction
Systems must be constructed of the following specifications: Crowns:
- Minimum framework thickness anterior: 0.4 mm
- Minimum framework thickness posterior: 0.6 mm Maryland-bridges:
- Minimum framework thickness anterior: 0.4 mm
- Minimum framework thickness posterior: 0.6 mm
- Connectors anterior: 6 mm²
- Connectors posterior: 9 mm²
- Minimum framework thickness posterior: 0.6 mm
- Connectors anterior: 6 mm²
- Connectors posterior: 9 mm²
Milling
Reduce feed rates during rough machining: The quality of milling depends on several factors including the machine, machining strategy, zirconium dioxide, etc. To ensure that you can achieve optimum milling results from the start with high translucence blanks, we recommend using a lower speed than with opaque materials during rough machining. Coated milling tools: These offer the benefit of low wear with longer tool life. Rough machining Occlusal/cavity:
- Tool diameter: 2.5 mm
- Spindle speed: 20,000-22,000 rpm
- Feed rate: 1,200-1,500 mm/min
- Infeed rate: 1,000 mm/min
- Allowance: 0.15 mm
- Tool path distance: 1.00 mm
- Step down/step over: 1.00 mm
- Spindle speed: 20,000-22,000 rpm
- Allowance: 0.15 mm
Adjustments
Any adjustments required to the sintered restorations once compacted must only be carried out using diamond-coated tools to prevent damage to the material caused by local overheating or exposure of the surface of the restoration to excessive force. Recommendation for standard sintering:
- Heating and cooling rate 10°C/min
- Hold time 120 minutes at 1,450°C
- Total sintering time approx. 7 hours Recommendation on rapid sintering: (for bridges with up to 3 pontics)
- Heating rate 10°C/min
- Hold time 30 minutes at 1,500°C
- Cooling rate 40°C/min
- Total sintering time approx. 4 hours Sintering together with other materials could cause unwanted changes in color and translucence. This applies particularly to materials processed using dye liquids. Sintering beads must also be replaced to avoid dye liquid residues. It is particularly important to clean sintering furnaces that are contaminated by dye liquids before sintering a pre-shaded material for the first time. This prevents unpleasant surprises and allows optimum photo-optical results for the zirconium dioxide.
Fixing
Restorations can be cemented conventionally with a zinc phosphate or glass ionomer cement or with self-adhesive and fully-adhesive fixing material.
Veneering
Any ceramic veneers recommended for zirconium dioxide ceramics may be used.
Our stable all-rounder
Supports you ideally on your individual route to highly esthetic and durable dentures. Can be used in all indications, available in all 16 VITA classic shades and additionally 3x bleach.
Votre sélection16 mm · B2
Informations produit
| Fabricant | Pritidenta GmbH |
|---|---|
| Teinte | B2 |
| Hauteur | 16 mm |
| Matériau | Zirconium dioxide Type II, Class 5 according to DIN EN ISO 6872 |
| Teintes disponibles | All 16 VITA classic shades and additionally 3x bleach |
| Hauteurs disponibles | 16 mm, 20 mm, 25 mm |
Documents de la gamme
- Link to the studyDocument